NPT Tap Drill Chart
Pick a pipe size to get the tap drill, threads per inch and pipe OD, with the hand-tight engagement and pitch diameters.
The NPT tap drill chart is a free, browser-based tool that gives the tap drill size for a National Pipe Taper (NPT) thread. Choose a pipe size from 1/16 to 4 in, and the result shows the tap drill, threads per inch, pipe outside diameter, and the thread values you need to set up the hole. It runs in your browser with no sign-up, and nothing you enter is uploaded. It also works on a phone, so you can check a drill size at the machine.
Use it when you drill and tap a port in a manifold, a tank fitting or a hydraulic block for a pipe fitting.
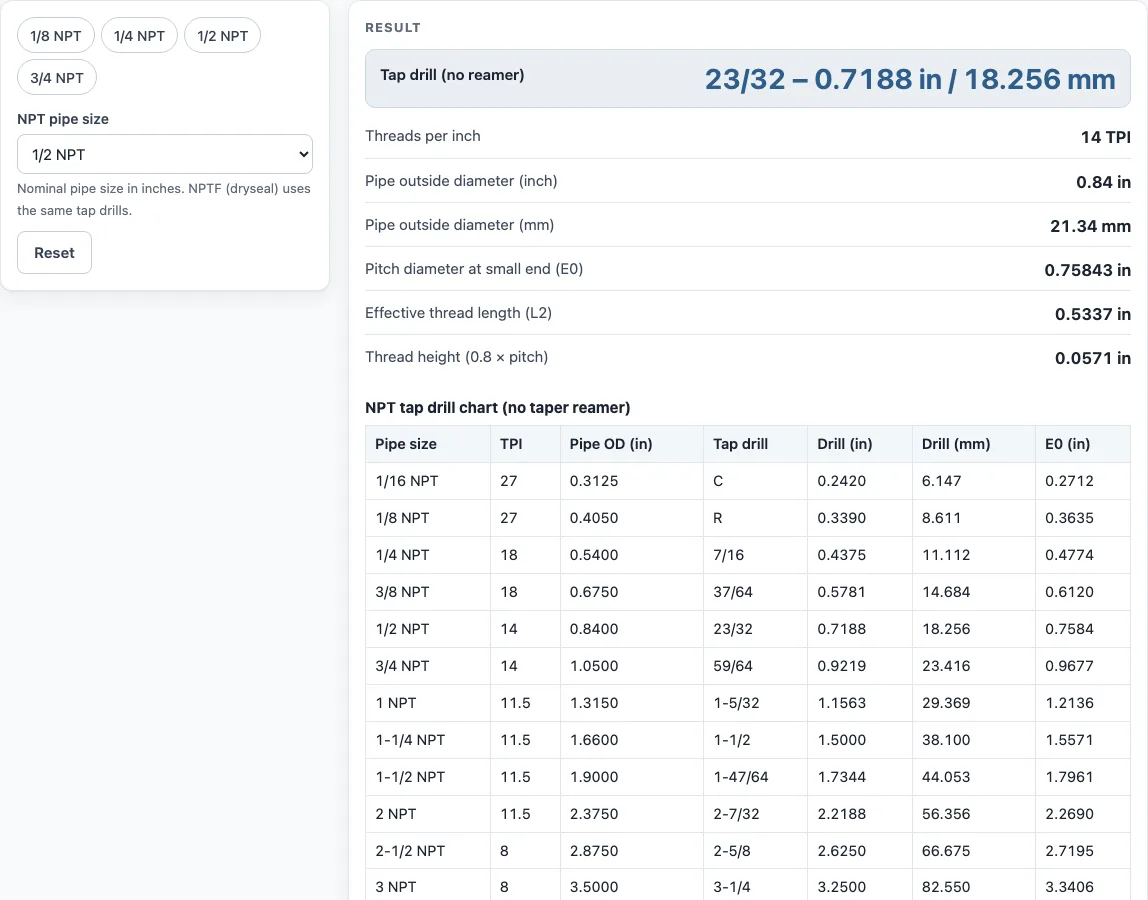
How to use the NPT tap drill chart
- Choose an NPT pipe size from 1/16 to 4 in.
- Read the tap drill in the result. This is the drill to use for holes tapped without a taper reamer.
- Check the threads per inch (TPI), the pipe outside diameter in inches and mm, the pitch diameter at the small end (E0), the effective thread length (L2), and the thread height.
- Scroll to the table under the result. It lists all 13 sizes with TPI, outside diameter, and drill size in inches and mm, so you can compare sizes.
- Open “How it was calculated” to see the formula and each step worked out with your numbers.
- Drill the hole with the tap drill, then tap it. Stop when the fitting reaches the right engagement. Check with a plug gauge or the mating fitting rather than tapping to a fixed depth.
Copy result copies the result lines with a link. Copy link copies the page address, which stores every input (?s=…), so opening it later restores the same calculation. Print / save as PDF prints the inputs, results, calculation steps, and the date.
The pipe size select lists every size from 1/16 to 4 NPT, and the presets jump straight to 1/8, 1/4, 1/2 and 3/4 NPT, the sizes used most in machine shops.
What size drill for a 1/4 NPT tap?
For a 1/4 NPT tap, drill a 7/16 hole, which is 0.4375 in or 11.112 mm. The 1/4 NPT threads are cut at 18 threads per inch.
The tap drill is smaller than the pipe’s outside diameter because the tap cuts the threads into the wall of the hole. The drill leaves enough material for the threads to form. NPT threads are tapered, narrowing by 1 in 16 on the diameter (3/4 in per foot), with a half angle of 1°47′ and a 60° thread angle. Because of the taper, the gauge dimensions are given at the small end of the pipe: E0 is the pitch diameter there.
The tool uses the ASME B1.20.1 formulas to find these values. With D as the pipe outside diameter (0.540 in for 1/4 NPT) and p as the pitch (1 ÷ 18 = 0.05556 in):
- E0 = D − (0.05 D + 1.1) p = 0.4774 in
- L2 = (0.80 D + 6.8) p = 0.4018 in
- Thread height h = 0.8 p = 0.0444 in
Why is a 1/2 NPT hole bigger than 1/2 inch?
A 1/2 NPT hole is not 1/2 inch across. The “1/2” is the nominal pipe size, not the diameter of the thread. A 1/2 NPT pipe has an outside diameter of 0.840 in, and that is the size the threads are built around.
This is why the tap drill for 1/2 NPT is 23/32 (0.7188 in), which is larger than 1/2 in. The same rule applies to every NPT size. The 1/4 NPT pipe is 0.540 in, and the 1 NPT pipe is 1.315 in. Always use the chart value for the tap drill, not the nominal size.
Is the NPTF tap drill the same as NPT?
Yes. NPTF (dryseal) threads use the same tap drills as NPT; the difference is in the crest and root fit that makes the dryseal thread seal without sealant. The tap itself is different, so use an NPTF tap when the drawing calls for NPTF.
Sources
- Engineers Edge, pipe thread tap and drill chart and National pipe thread (Wikipedia) — NPT drills without a taper reamer, pipe outside diameters and L2
- Allied Machine tap drill chart — C drill (0.242 in) for 1/16-27 NPT without a reamer
- ASME B1.20.1 formulas E0 = D − (0.05 D + 1.1) p and L2 = (0.80 D + 6.8) p, thread height 0.8 p, taper 1:16
Worked examples
| Input | Result |
|---|---|
| 1/8 NPT | tap drill R (0.3390 in / 8.611 mm), 27 TPI |
| 1/4 NPT | tap drill 7/16 (0.4375 in / 11.112 mm), 18 TPI |
| 1/2 NPT | tap drill 23/32 (0.7188 in / 18.256 mm), 14 TPI |
| 3/4 NPT | tap drill 59/64 (0.9219 in / 23.416 mm), 14 TPI |
| 2 NPT | tap drill 2-7/32 (2.2188 in / 56.356 mm), 11.5 TPI |
Calculated by the tool above with these values.
Frequently asked questions
What is the tap drill for 1/8 NPT?
The tap drill for 1/8 NPT is R, which is 0.339 in or 8.611 mm. The threads are cut at 27 threads per inch.
What drill size for 1/2 NPT?
Use a 23/32 drill for 1/2 NPT, which is 0.7188 in or 18.256 mm. The threads are 14 per inch.
What drill size for a 1 inch NPT tap?
The tap drill for a 1 inch NPT tap is 1-5/32, and the threads are 11.5 per inch. The pipe outside diameter for 1 NPT is 1.315 in. Check the decimal and mm values in the result before you buy the drill.
How many threads per inch does NPT use?
NPT uses 27 threads per inch for 1/16 and 1/8, 18 for 1/4 and 3/8, and 14 for 1/2 and 3/4. From 1 to 2 in, it uses 11.5 per inch, and 8 per inch for 2-1/2 in and larger.
Can I use the results in shop documents?
Yes. Results may be used in commercial work, including quotes, shop travelers, setup sheets, inspection reports, and customer documents, without attribution.
Do I need a taper pipe reamer?
No. The drills listed are for holes tapped straight from the drill, without a reamer. If you ream the hole with a taper pipe reamer first, a smaller drill is used; take that size from the tap or reamer maker’s data.
How deep do I tap an NPT hole?
Tap until the fitting reaches the right engagement rather than to a fixed depth, and check with an NPT plug gauge or the mating fitting. The effective thread length L2 in the result shows how much thread a pipe of that size carries.
Related tools
- Drill and tap chart – Use it to compare tap drill sizes for other thread types beyond NPT.
- Drill size chart – Use it when you need the drill size for a plain hole rather than a tapped one.
- Taper angle calculator – Use it when you need the angle of a tapered part, such as the NPT taper.
- Thread pitch calculator – Use it for the pitch and minor diameters of straight (parallel) threads.
- Decimal to fraction inches – Use it to convert a decimal drill size to its nearest fraction.
- All machining calculators – Use it to browse every calculator on the site.