Drill and Tap Chart (Tap Drill Calculator)
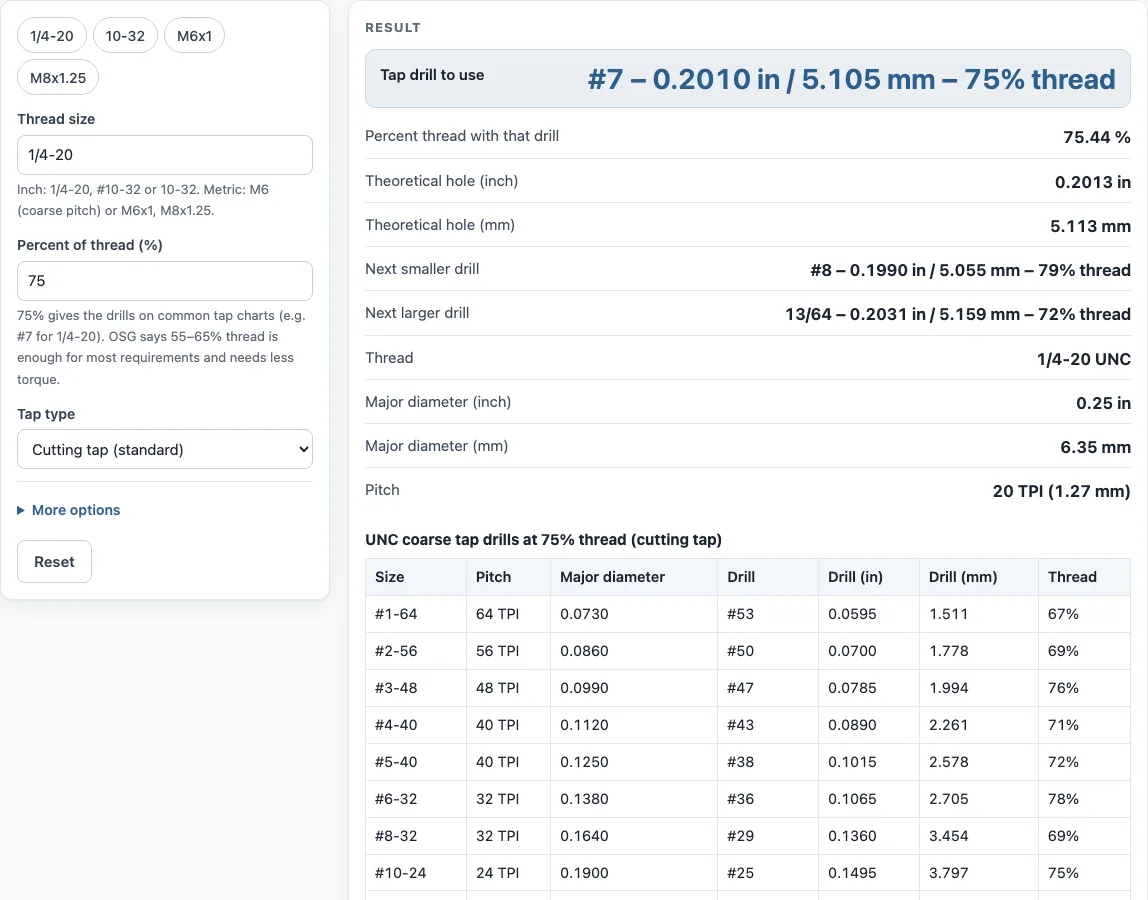
Type a thread such as 1/4-20 or M6x1 to get the tap drill size and the % of thread it cuts; the full chart for the series is below.
Popular tools
How to use the drill and tap chart
- Type the thread size in the Thread size box. Inch sizes look like 1/4-20, #10-32 or 10-32. Metric sizes look like M6 or M6x1.
- For a metric size outside the coarse list, type the pitch, such as M12x1.25. Without a pitch, M6 is assumed to be coarse.
- Choose the tap type: cutting tap or forming (roll) tap.
- Check Percent of thread. It defaults to 75%, which gives the drills found on common tap charts, such as #7 for 1/4-20. OSG, a tap maker, says a 55–65% thread is enough for most requirements and needs less tapping torque.
- Set Drills allowed to match the thread, inch only, metric only, or all drill sets.
- Read the result. It shows the closest standard drill, its actual % thread, the theoretical hole in inches and mm, and the next smaller and next larger drills with their % thread.
- Check for warnings. A cutting tap warns outside 50–85% thread, and a forming tap warns outside 55–80%.
- Scroll down to the full chart for the series you selected.
- Open How it was calculated to see the formula with your numbers.
Copy result copies the result lines with a link. Copy link copies the page address, which stores every input, so opening it later restores the same calculation. Print / save as PDF prints the inputs, results, calculation steps and the date.
What size drill for a 1/4-20 tap?
For a 1/4-20 cutting tap at 75% thread, the closest standard drill is #7. It measures 0.2010 in (5.105 mm) and gives 75.4% thread. The “1/4” is the major diameter, and “20” is the number of threads per inch (TPI). Always check the result against your own percent, because a different percent can change the closest drill.
How do you calculate tap drill size?
For inch threads, the cutting tap formula is tap drill = major diameter − 0.01299 × % thread ÷ TPI. For metric threads, it is major diameter − % thread × pitch ÷ 76.98. Both give the same result as major − 1.299 × pitch × % ÷ 100.
For example, a 10-32 thread has a major diameter of 0.190 in. At 75%, the calculation is 0.190 − (0.01299 × 75 ÷ 32), which equals about 0.1596 in. The closest standard drill is #21 (0.1590 in), which gives 76.4% thread. The tool shows each of these steps under “How it was calculated.”
What is percent of thread?
Percent of thread is how much of the full thread depth the tap cuts into the hole wall. A higher percentage gives a stronger thread but needs more tapping torque. A smaller drill means more thread engagement and more torque, while a larger drill means less engagement.
A higher percent of thread takes more tapping torque. OSG’s tap drill chart advises using the largest drill that still gives adequate strength, and says a 55–65% thread is sufficient for most requirements. Its table suggests about 60–70% for iron and mild steel and 75–85% for thin sheet.
What drill do I use for a forming (roll) tap?
A forming tap uses a larger hole than a cutting tap, because it displaces metal instead of cutting it. The forming formula is major diameter − 0.0068 × % thread ÷ TPI. For inch threads, this gives a larger drill for the same thread.
For a 1/4-20 forming tap at 65% thread, the closest standard drill is #1, which measures 0.2280 in (5.791 mm) and gives 64.7% thread. Confirm the drill size with the tap maker’s chart for your material, since the right hole size depends on the material being tapped.
What tap drill for M6x1 and M8x1.25?
For an M6x1 cutting tap at 75%, the drill is 5.0 mm (0.1969 in), which gives 77% thread. For an M8x1.25 cutting tap at 75%, the drill is 6.8 mm (0.2677 in), which gives 73.9% thread.
For metric coarse threads at 75%, the drill is close to the major diameter minus the pitch. M6x1 gives 6 − 1 = 5 mm, and M8x1.25 gives about 6.75 mm, which rounds to the 6.8 mm standard drill.
Metric drill and tap guide chart
The chart under the calculator is a complete tap drill guide for one thread series at a time. Choose UNC, UNF, metric coarse or metric fine under Chart below the result to switch it; for metric threads it lists every size from M1 to M30 (coarse) with the drill in mm and inches. Whether you call it a tap and die drill chart, a drill bit size chart for taps or a tap and drill table, it answers the same question: which drill bit size goes with which tap size. Each row gives the tap dimensions (thread size, pitch and major diameter) and the drill dia for tapping, so you can read the drill bit size straight from the tap size.
Sources
- OSG tap drill size chart (2024) — drill = major − 0.01299 × % ÷ TPI, 55–65% thread for most requirements
- Dormer forming taps data sheet — forming-tap hole D = D nom − 0.0068 × P × %
- Unified Thread Standard (Wikipedia) — UNC and UNF threads per inch (ASME B1.1)
- ISO metric screw thread (Wikipedia) — ISO 261 coarse and fine pitches and the ISO 68-1 basic profile
- Drill bit sizes (Wikipedia) — number and letter drill decimals of ASME B94.11M, checked size by size
Worked examples
| Input | Result |
|---|---|
| 1/4-20, 75% thread, cutting tap | drill #7 (0.2010 in / 5.105 mm), 75.4% thread |
| 10-32, 75% thread, cutting tap | drill #21 (0.1590 in / 4.039 mm), 76.4% thread |
| M6x1, 75% thread, cutting tap | drill 5.0 mm (0.1969 in / 5.000 mm), 77% thread |
| M8x1.25, 75% thread, cutting tap | drill 6.8 mm (0.2677 in / 6.800 mm), 73.9% thread |
| 1/4-20, 65% thread, forming tap | drill #1 (0.2280 in / 5.791 mm), 64.7% thread |
Calculated by the tool above with these values.
Frequently asked questions
What size drill for a 6-32 tap?
For a 6-32 cutting tap at 75% thread, the closest standard drill is #36, which measures 0.1065 in. Check the actual % thread shown in the result if you use a different percent.
Can I print the drill and tap chart?
Yes. Use Print / save as PDF to print the inputs, results, calculation steps and the date. You can also save the same output as a PDF.
Is it free, and is anything uploaded?
Yes, the tool is free and needs no sign-up. Everything runs in your browser, and nothing is uploaded.
What drill do I use for a 3/8-16 tap?
At 75% thread for a cutting tap, the closest standard drill for a 3/8-16 thread is 5/16. Compare the next smaller and next larger drills if you need a different percent.
What tap drill do I use for an M10x1.5 thread?
At 75% thread for a cutting tap, the closest standard drill for M10x1.5 is 8.5 mm. The result shows the actual percent of thread that drill gives.
What if my thread size is not in the list?
Sizes outside the standard lists still work. For metric sizes outside the coarse list, type the pitch, such as M12x1.25, so the calculator can use the correct value.
Can I use the results in customer documents?
Yes. Results may be used in commercial work, such as quotes, shop travelers, setup sheets, inspection reports and customer documents, without attribution.
Related tools
- Drill size chart: Use it to compare drill sizes in fractions, numbers, letters and mm.
- NPT tap drill chart: Use it when you are working with NPT pipe threads.
- Thread pitch calculator: Use it for the pitch diameter, minor diameters and thread depth of the same thread.
- Decimal to fraction inches: Use it to convert a decimal drill size to the nearest fraction.
- Countersink depth calculator: Use it to find how deep to cut a countersink.
- Speeds and feeds calculator: Use it to set spindle speed and feed rate for the drilling operation before you tap.
- Machine screw size chart: Use it to see the diameter, thread pitches and tap drill of a number-size screw.
- All machining calculators: Use it to browse every calculator on the site.